Call us now :08037735925
 Send Inquiry

 Send Inquiry
Double Effect Forced Circulation Evaporator
Price 1000000 INR/ Piece
MOQ : 1 Piece
Double Effect Forced Circulation Evaporator Specification
- Usage & Applications
- Water Recovery
- Automation Grade
- Automatic
- Temperature
- Max 130 Deg C
- Product Type
- Double Effect Forced Circulation Evaporator
- Material
- Stainless Steel 316L
- Capacity
- 7501-10000LPH
- Voltage
- 415 V
- Deal Status
- New Only
- Circulation Mode
- Forced Circulation
- Condensate Recovery
- Integrated System
- Heating Source
- Steam Driven
- Pressure Range
- Atmospheric to 1.5 Bar
- Feed Capacity
- 500 KLD
- Evaporation Stages
- Double Effect
- Structure Type
- Vertical Design
Double Effect Forced Circulation Evaporator Trade Information
- Minimum Order Quantity
- 1 Piece
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10 Pieces Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
Double Effect Forced Circulation Evaporator About
Discover the astounding efficiency of our Double Effect Forced Circulation Evaporator, crafted for industries seeking sublime water recovery and process optimization. With a robust feed capacity of 500 KLD and an evaporation range of 7501-10000 LPH, this vertical, stainless steel 316L structure ensures excellence in thermal performance. Utilise its integrated condensate recovery and steam-driven heating for maximal resource utilization. Certified, new, and automatic, this in-demand solution offers remarkable durability across atmospheric to 1.5 Bar pressure. Find commercial and industrial solutions from a trusted exporter, manufacturer, and supplier in India!
Commercial Use & Versatile Plant Applications
Engineered for excellence, our Double Effect Forced Circulation Evaporator finds widespread use in commercial water recovery and process plants. Its general utility spans across industries such as chemicals, pharmaceuticals, and wastewater treatment, ensuring efficient evaporation and resource reuse. This system brings sublime performance to any plant application, delivering reliable operation, minimal maintenance, and high yield efficiencies. Designed for both specific operational needs and broader industrial use, it greatly enhances production value wherever it's deployed.
Supply Ability & Export Credentials
Our Double Effect Forced Circulation Evaporators are regularly dispatched and handed over to clients worldwide at the lowest price, thanks to our robust export infrastructure. We proudly serve markets in Asia, the Middle East, Africa, and Europe, maintaining a consistent supply chain driven by excellence. Holding internationally recognized certifications, our units guarantee reliability, safety, and quality. These standards ensure customers receive a solution that meets global demands, fulfilling commercial and industrial requirements across varied geographies.
Commercial Use & Versatile Plant Applications
Engineered for excellence, our Double Effect Forced Circulation Evaporator finds widespread use in commercial water recovery and process plants. Its general utility spans across industries such as chemicals, pharmaceuticals, and wastewater treatment, ensuring efficient evaporation and resource reuse. This system brings sublime performance to any plant application, delivering reliable operation, minimal maintenance, and high yield efficiencies. Designed for both specific operational needs and broader industrial use, it greatly enhances production value wherever it's deployed.
Supply Ability & Export Credentials
Our Double Effect Forced Circulation Evaporators are regularly dispatched and handed over to clients worldwide at the lowest price, thanks to our robust export infrastructure. We proudly serve markets in Asia, the Middle East, Africa, and Europe, maintaining a consistent supply chain driven by excellence. Holding internationally recognized certifications, our units guarantee reliability, safety, and quality. These standards ensure customers receive a solution that meets global demands, fulfilling commercial and industrial requirements across varied geographies.
FAQ's of Double Effect Forced Circulation Evaporator:
Q: How does the Double Effect Forced Circulation Evaporator improve water recovery in industrial plants?
A: The system utilizes a double-effect evaporation process, significantly increasing efficiency by reusing heat between stages and ensuring maximum recovery of water from industrial effluents.Q: What are the primary commercial uses for this evaporator model?
A: Its excellent design makes it ideal for chemical, pharmaceutical, and wastewater treatment plants, providing a sublime solution for concentrating solutions and recovering valuable resources.Q: Where can this evaporator be installed?
A: The vertical, forced circulation design allows for flexible installation in a variety of plant layouts, including new or existing production facilities requiring efficient evaporation processes.Q: When should industries consider utilizing this evaporator?
A: It is most beneficial when there is a need for high-capacity water recovery, especially for processes demanding robust operation under pressures up to 1.5 Bar and temperatures up to 130C.Q: What benefits do clients gain from the integrated condensate recovery system?
A: Clients find that condensate reuse reduces freshwater consumption, offers cost savings, and boosts overall system efficiency, aligning with sustainable practices.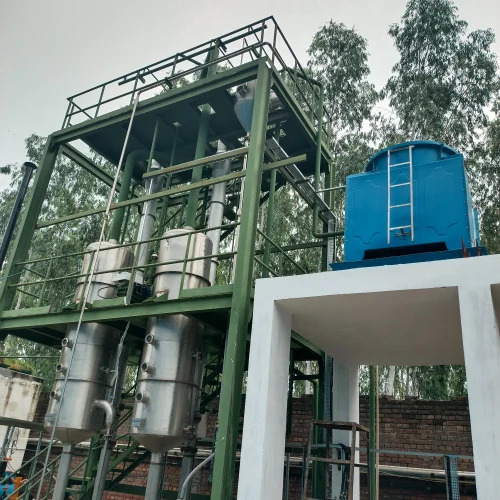
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Air Pollution Control Device Category

Wet Scrubber For Boiler
Price 880000 INR / Piece
Minimum Order Quantity : 1 Piece
Usage & Applications : Boiler flue gas treatment
Material : Stainless Steel
Automation Grade : Semi Automatic
Product Type : Wet Scrubber For Boiler

Bag Filter House
Price 475000 INR / Piece
Minimum Order Quantity : 1 Piece
Usage & Applications : Industrial, Food Industry
Material : MS
Automation Grade : Semi Automatic
Product Type : Bag Filter House
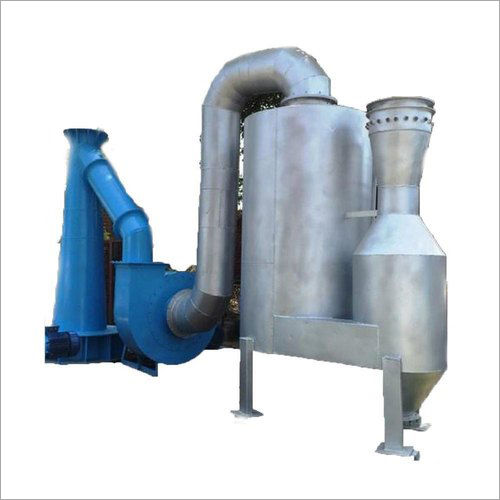
Venturi Scrubber
Price 400000 INR / Plant
Minimum Order Quantity : 1 Plant
Usage & Applications : Fume / Dust Extraction
Material : Mild Steel

CEME 60 Anti Smog Gun
Price 430000 INR / Piece
Minimum Order Quantity : 1 Piece
Usage & Applications : Pollution Control
Material : Mild Steel
Automation Grade : Fully Automatic
Product Type : Anti Smog Gun

 Send Inquiry
Our Products
- Effluent Treatment Plant
- Sewage Treatment Plant
- Filtration Unit
- Water Treatment Chemical
- Axial Fan
- Wastewater Treatment Plant
- Effluent Treatment & Wastewater Treatment Plant
- Waste Water Treatment Plant
- Zero Liquid Discharge
- Reverse Osmosis Plant
- Greywater Treatment Plant
- Waste Water Treatment
- Air Pollution Control System
- Air Pollution Control Device


Samathal - Hashampur Gopal, SEZ Road, Pakbada,Moradabad - 244001, Uttar Pradesh, India

Mr. Chandra Mohan Srivastav
(C.E.O.)
Mobile :08037735925
 Send Inquiry
 Send SMS
 Call Me Free

Developed and Managed by Infocom Network Private Limited.


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
